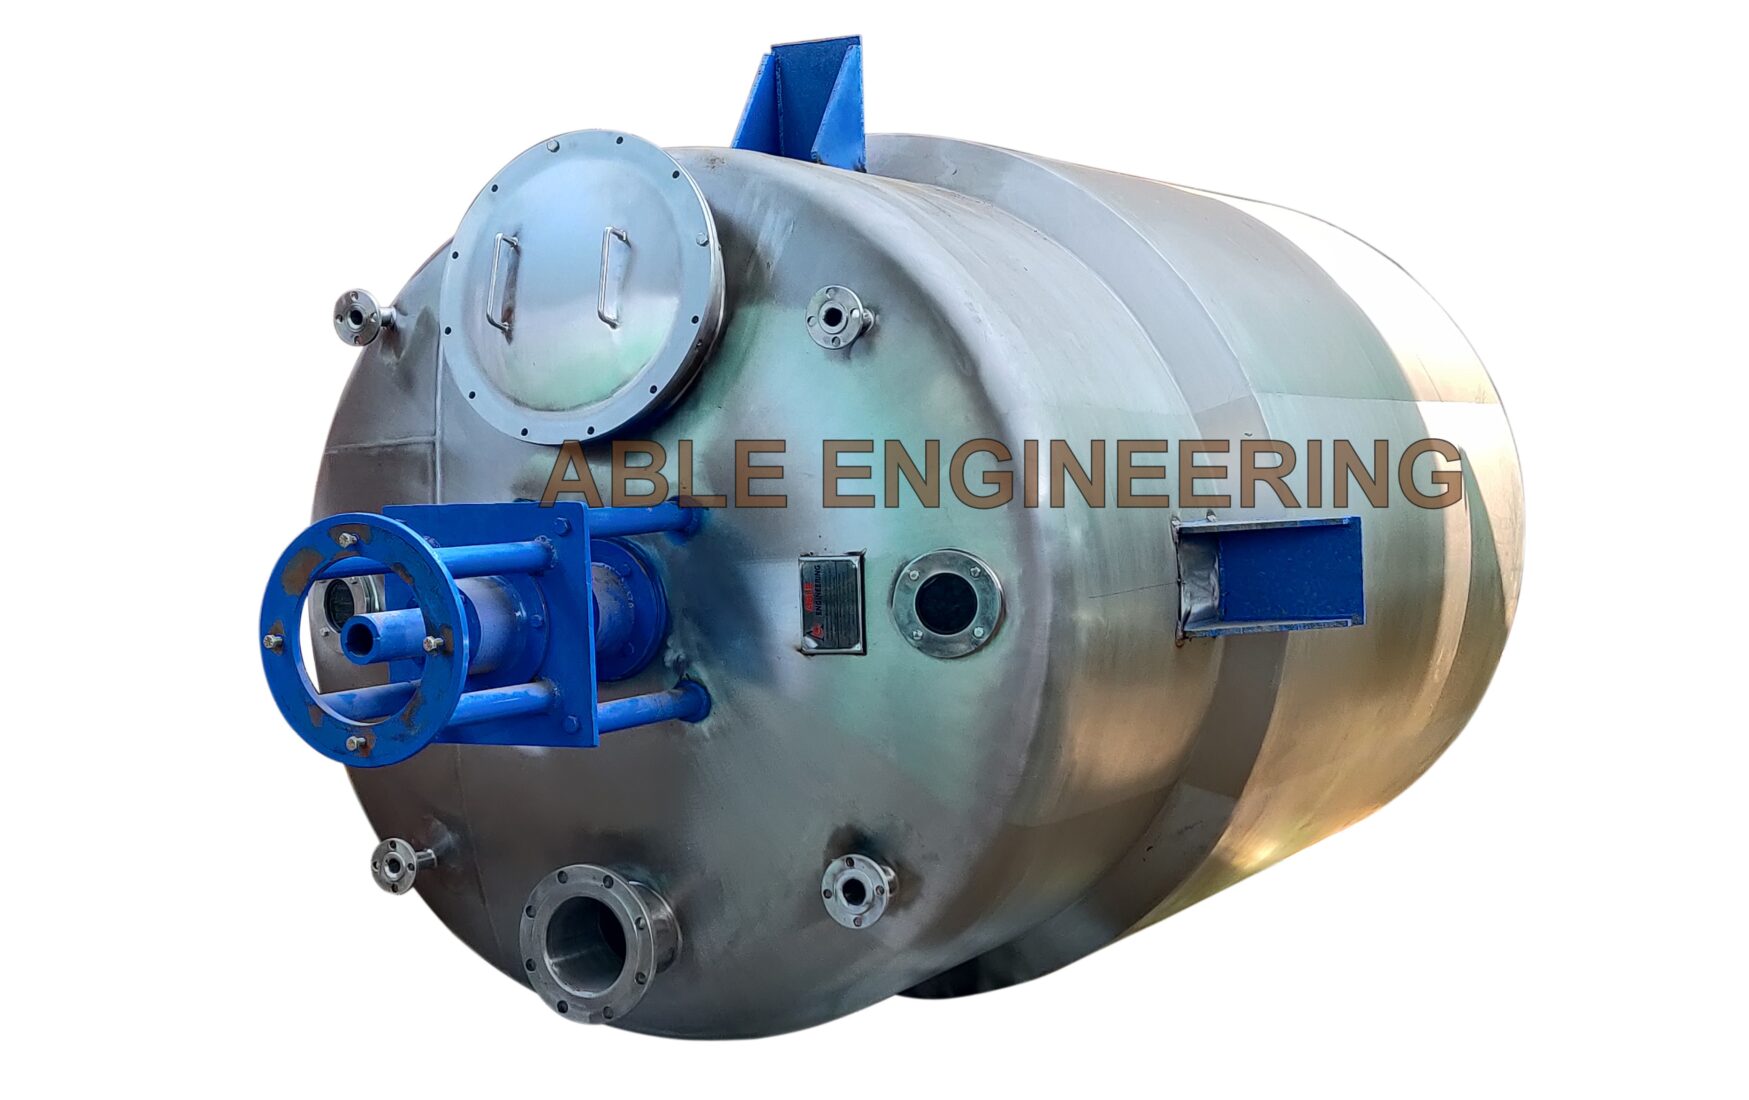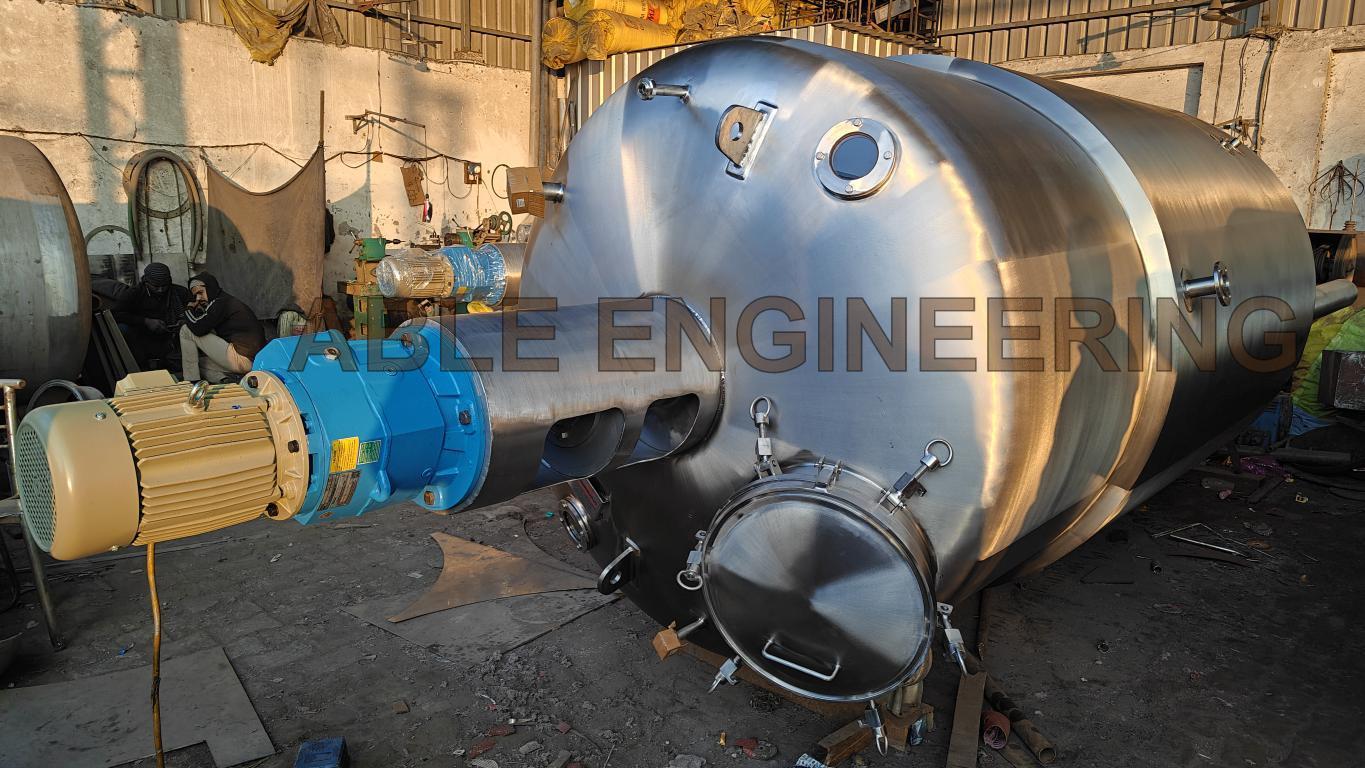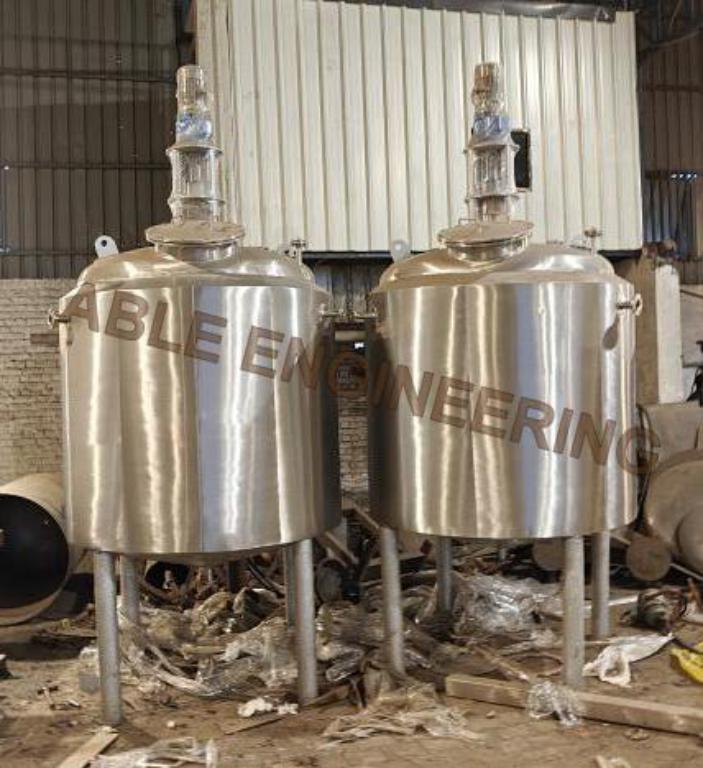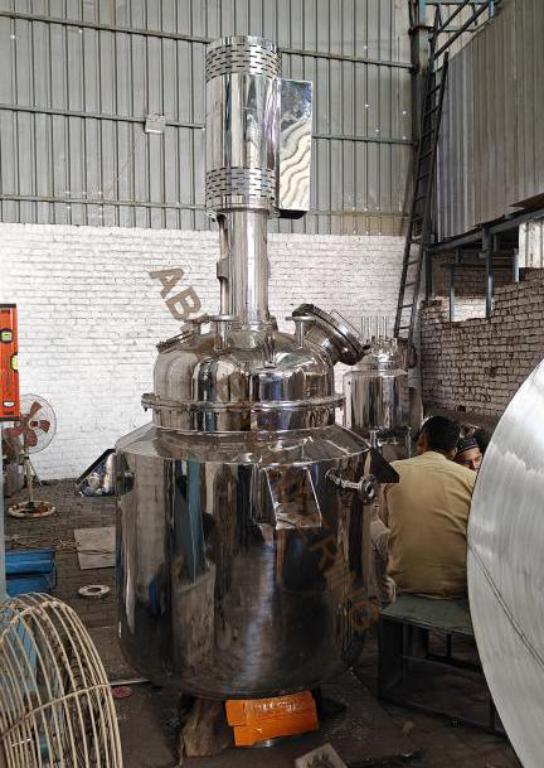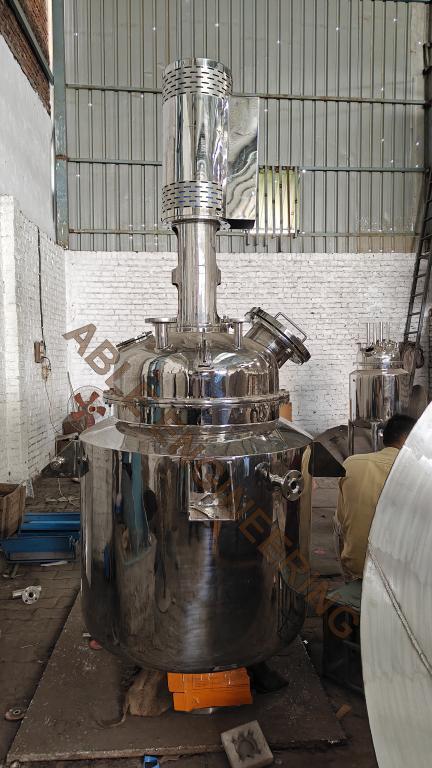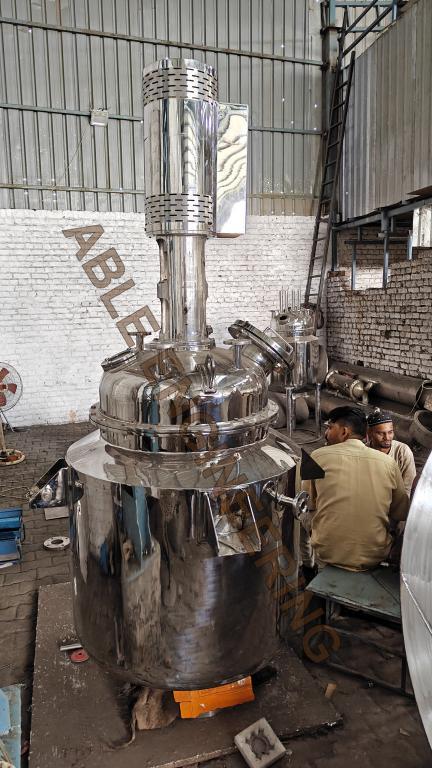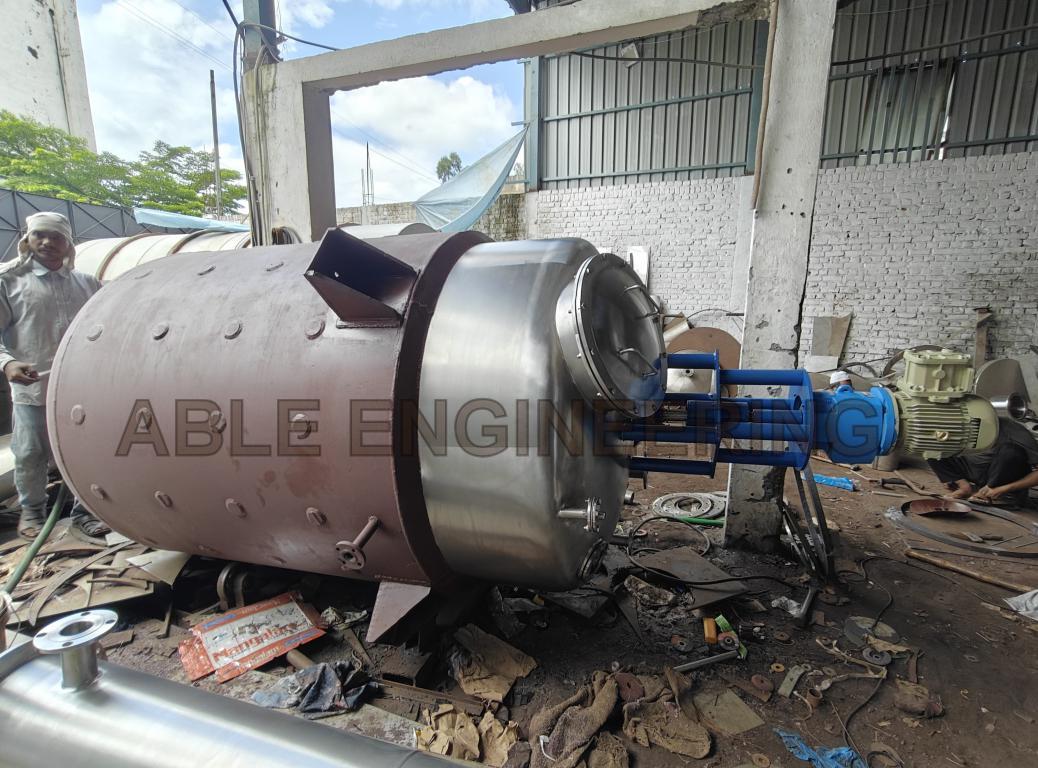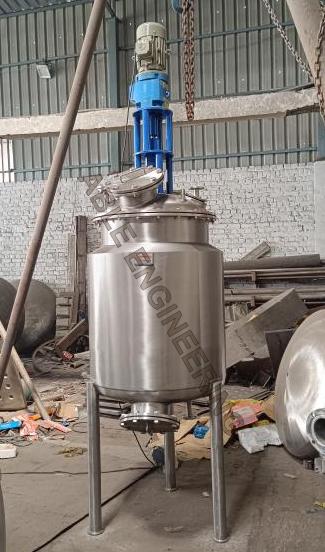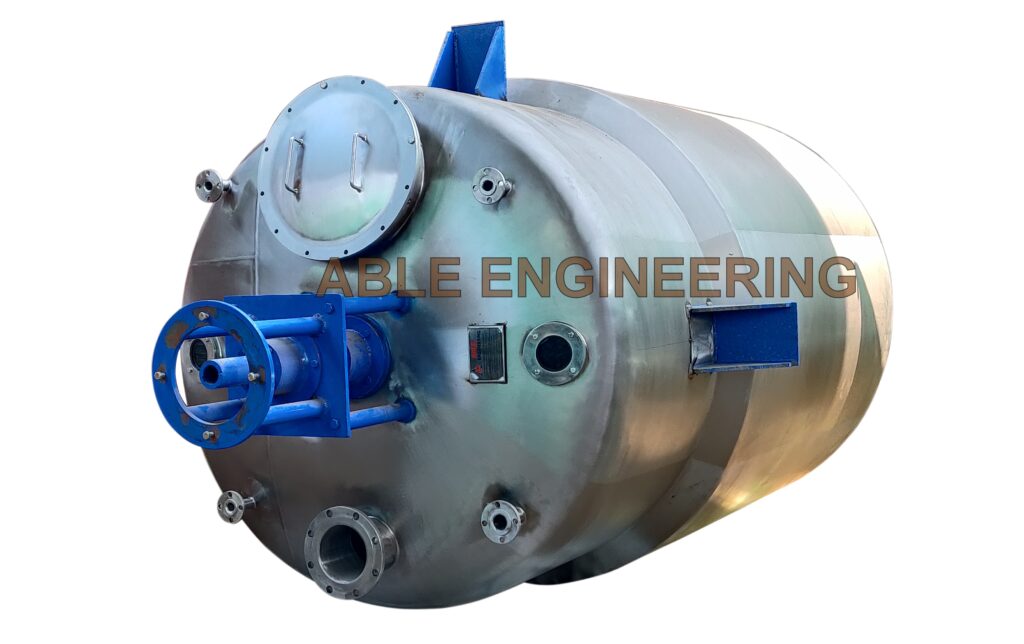
Chemical Reactor
Industrial chemical reactors designed for controlled processing and chemical reactions. Available with different agitator configurations and customized to suit your process requirements.
Capacity100 L – 15000 L
MaterialSS 316L / SS 304
Agitator TypesAnchor, Propeller, Paddle, Pitched-Blade Turbine
Mixing OptionHigh-Speed Homogenizer, where required
Engineered for your process.
Our chemical reactors are designed for a wide range of industrial reaction processes. Depending on your application, they can be configured with anchor, propeller, paddle or pitched-blade turbine agitators to suit different mixing requirements.
Multiple Agitator Options
Custom-Built to Your Requirements
Stainless Steel Construction
Designed for Industrial Processing
Technical specifications
Reactor configurations and specifications are finalized according to your process, capacity and material requirements.
| Capacity | 100 L – 15000 L |
|---|---|
| Material | SS 316L / SS 304 |
| Agitator Types | Anchor, Propeller, Paddle, Pitched-Blade Turbine |
| Mixing Option | High-Speed Homogenizer, where required |
| Design pressure | FV to 10 bar |
| Finish | Mirror / Matt |
| Standards | cGMP |
| Customization: As per process requirements |
Where it's used
Chemical reactors are used for a variety of industrial reactions and processing operations across multiple industries.
Herbal Extraction PlantsPharmaceutical PlantsChemical PlantsCondensationPolymerizationEsterificationHydrolysisOxidation and Reduction
Scroll · 1 / 4